Ancorite provides a comprehensive range of ancillary items to support the design and installation of flooring systems, ensuring a complete and high-performing solution for industrial and commercial environments. From stainless steel drainage systems to screeds and wall coatings, we deliver tailored services to meet the unique needs of our clients.
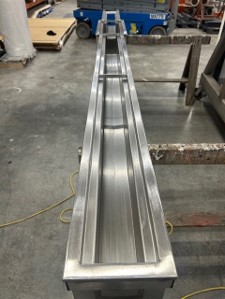
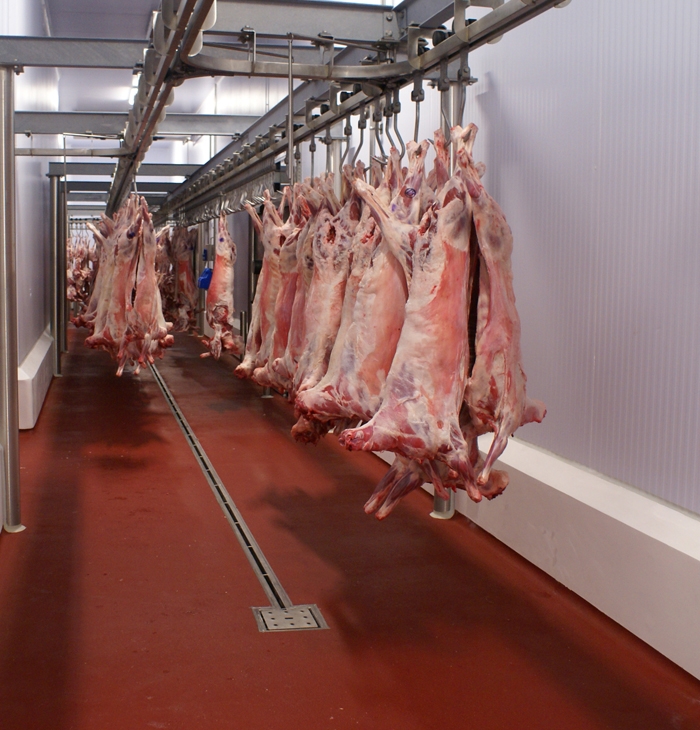
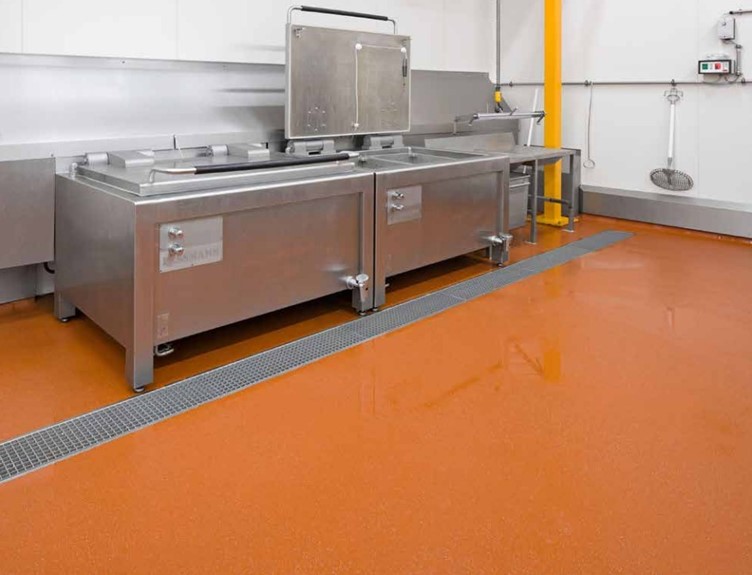
Ancorite can specify, supply and install stainless steel gullies and channels and these can be manufactured to order. We also offer a range of stainless-steel skirts and kerbs which are especially popular with the food industry. We have an extensive range of suppliers including Dunelm, Blucher, Aco and Defabs.
Ancorite can also supply and install a range of screeds from thin cementitious self levelling screeds to concrete and polymer or fibre modified screeds laid to falls. These can be used for tiling or as an underlay for other floor finishes.
Ancorite can apply a range of epoxy, acrylic and polyurethane wall coatings. These include decontaminated reinforced laminate systems for Pharmaceutical Clean Rooms, Operating Theatres and Kitchens
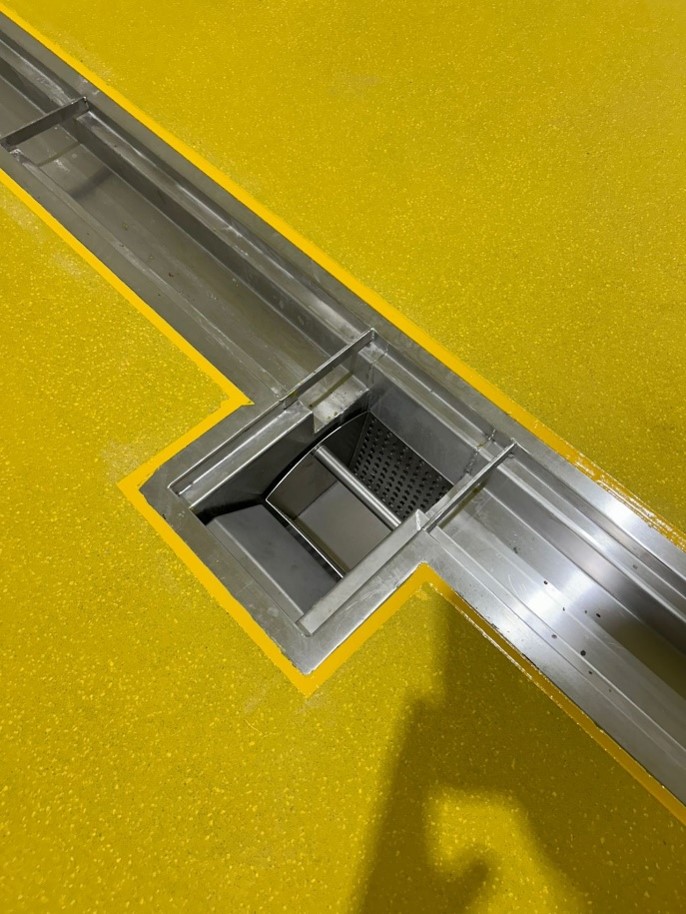
Ancorite provides ancillary systems designed to work alongside industrial flooring installations, including stainless steel drainage, screeds, kerbs, skirts and specialist wall coatings. These components can be specified as part of an integrated solution for demanding environments where hygiene, drainage, durability and ease of maintenance are critical.
Ancillary items are supporting components used alongside industrial flooring systems to ensure a complete, high-performance installation.
These typically include drainage systems, screeds, and wall coatings, all of which play a critical role in improving durability, hygiene, and overall system performance in demanding industrial environments.
Ancillary items are essential to ensure the flooring system performs as intended over the long term. They address key factors such as drainage, correct substrate preparation, and hygiene requirements.
Without properly specified ancillary components, even high-quality flooring systems may fail to meet operational demands, safety standards, or compliance requirements within industrial environments.
Ancorite installs a wide range of ancillary items including stainless steel drainage systems, levelling and modified screeds, and specialist wall coatings.
Each component is selected and installed to support the specific operational conditions of the facility, ensuring the flooring system performs reliably under heavy-duty use.
Screeds are used to level and prepare the substrate before the final flooring system is applied, providing a stable and even base.
They can also be designed to improve drainage, accommodate falls, and support heavy-duty applications, ensuring the finished system performs effectively under operational loads.
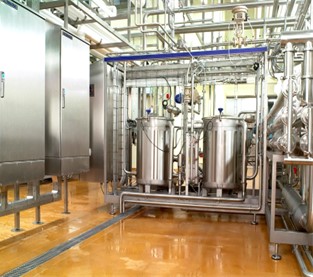
Ancillary flooring systems are commonly used in industries such as food and beverage, pharmaceutical, chemical processing, and manufacturing.
These environments require fully integrated flooring solutions that support hygiene, effective drainage, and long-term durability under demanding operating conditions.