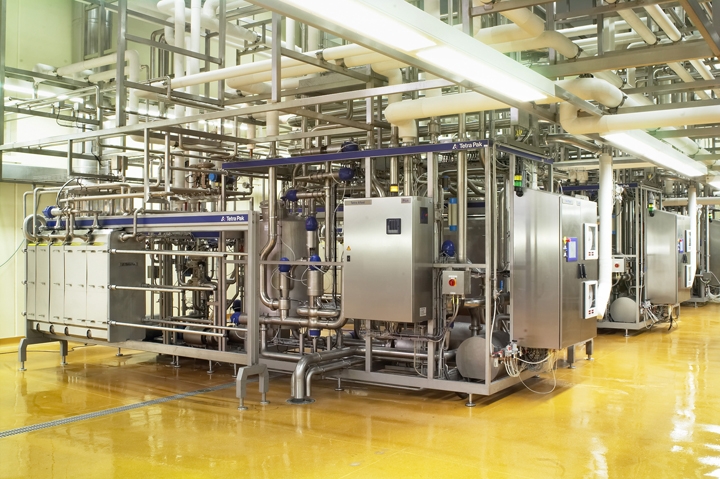
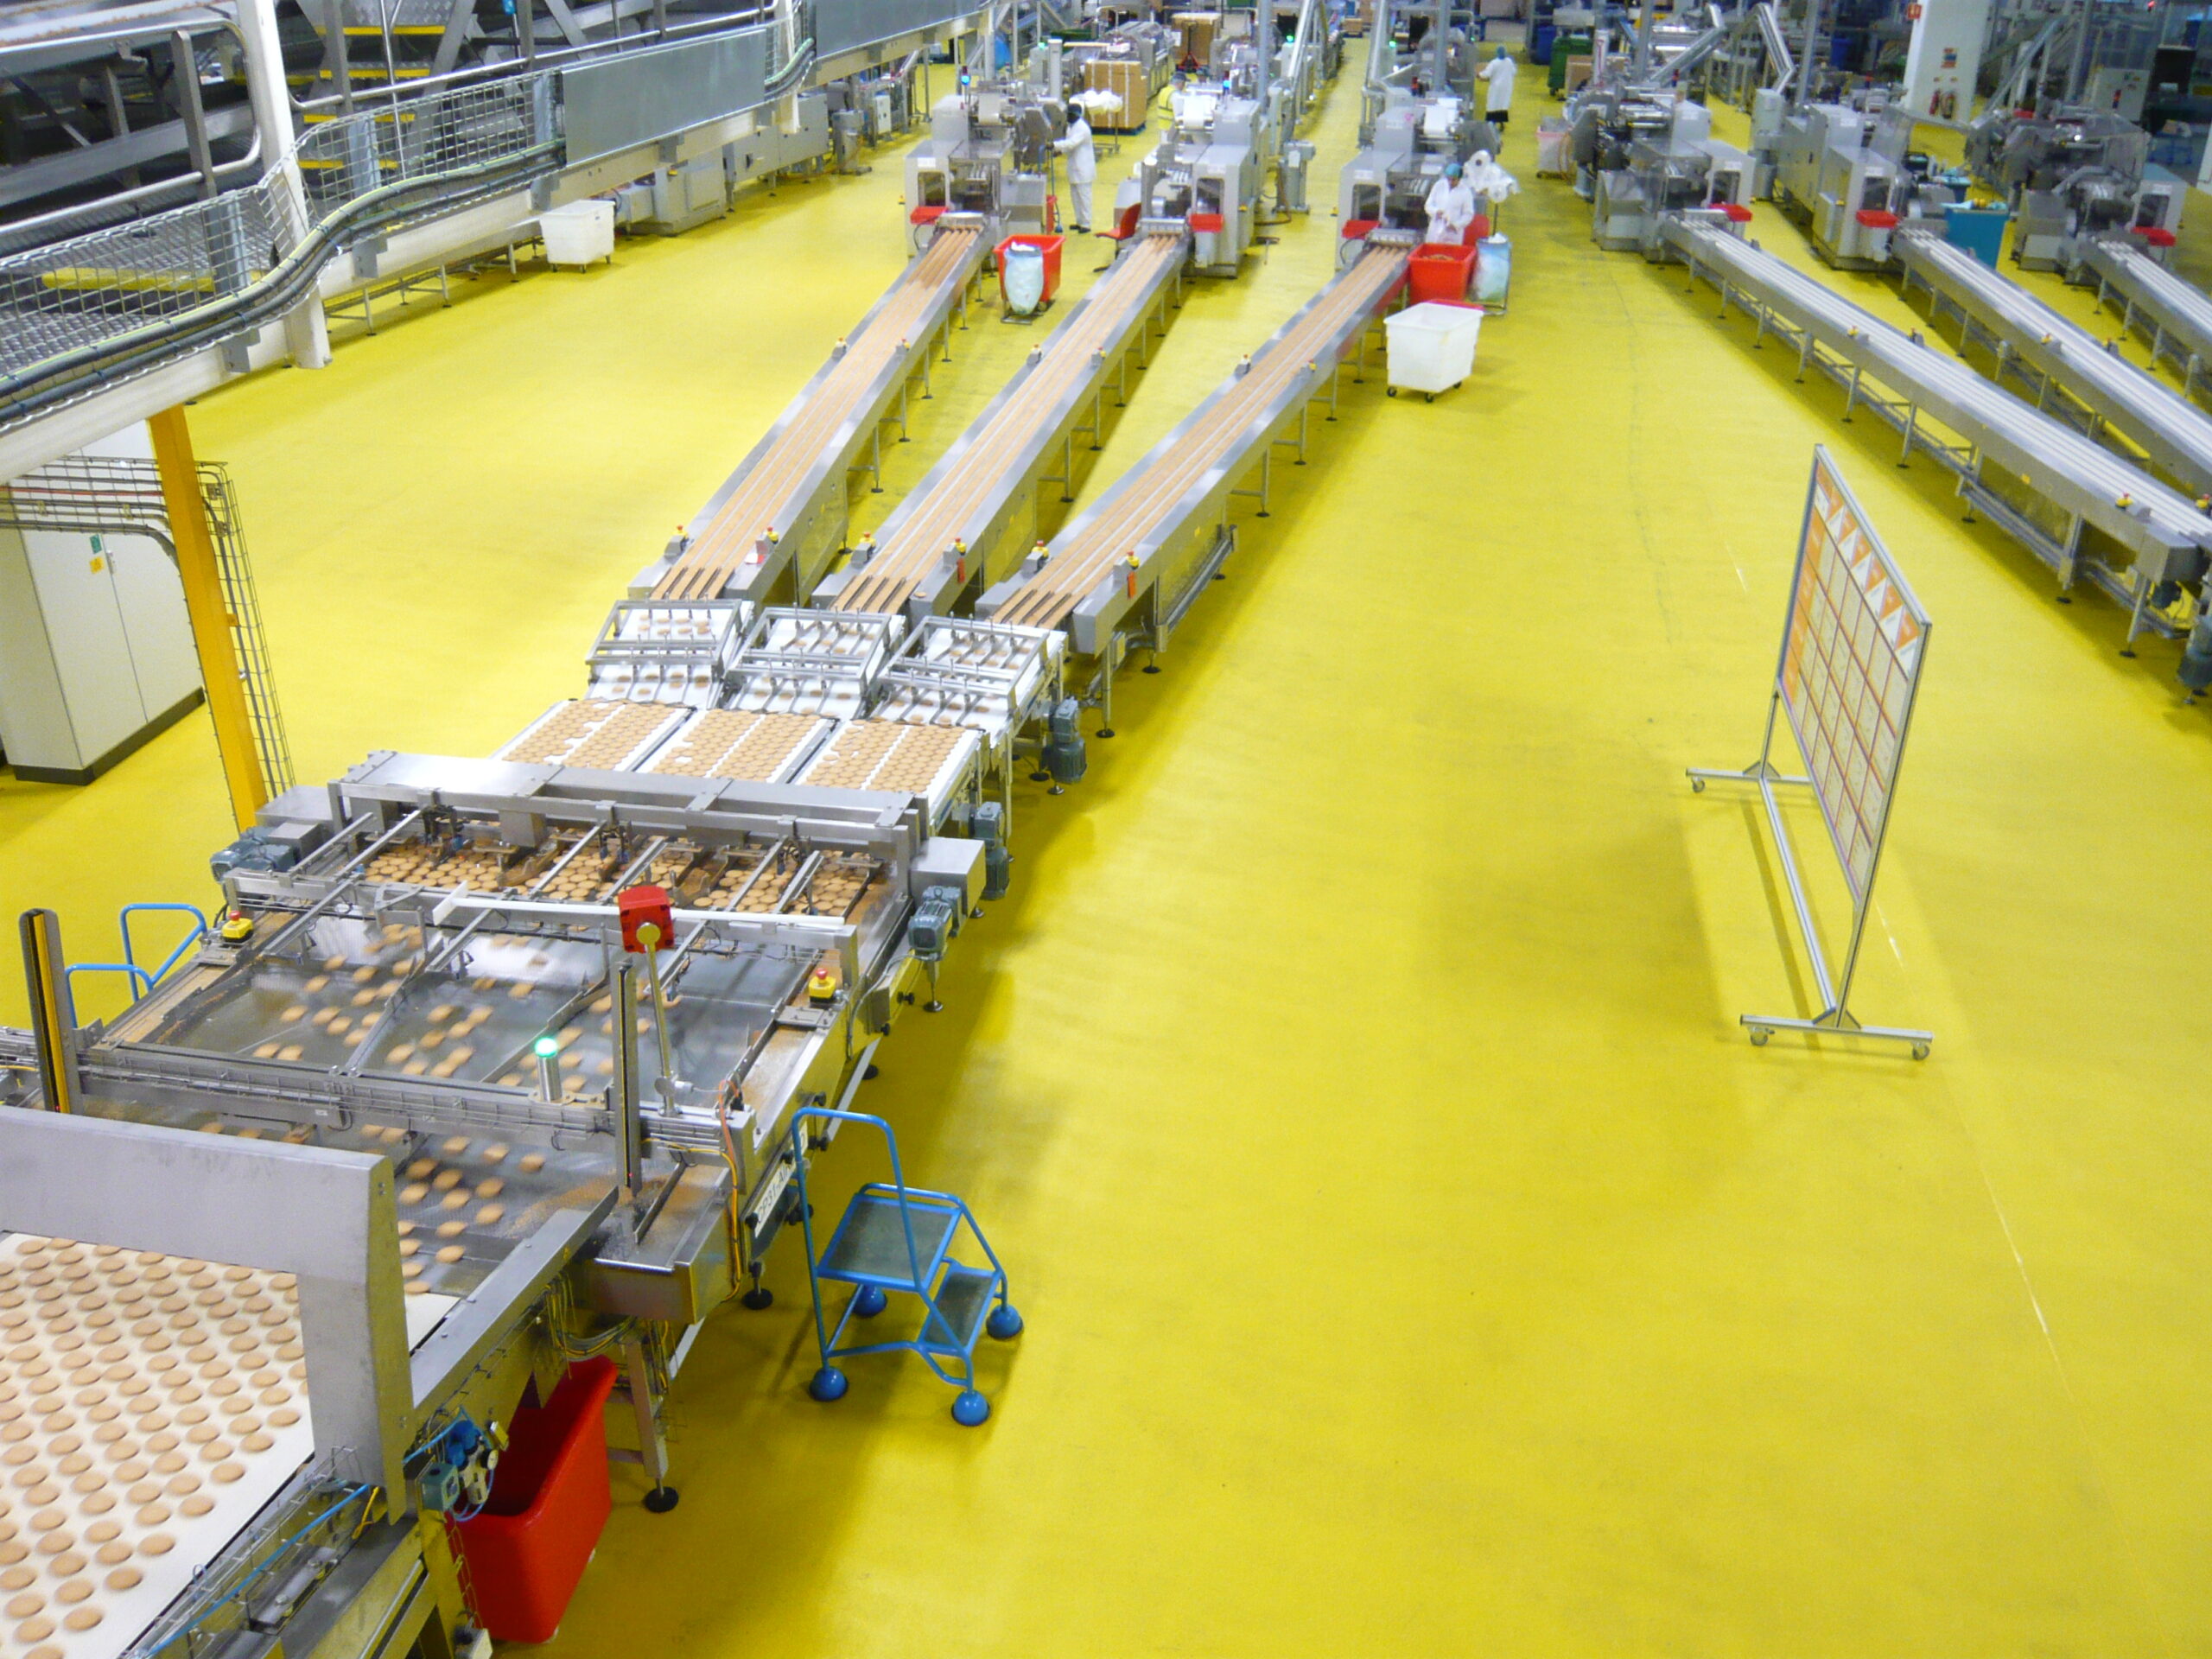
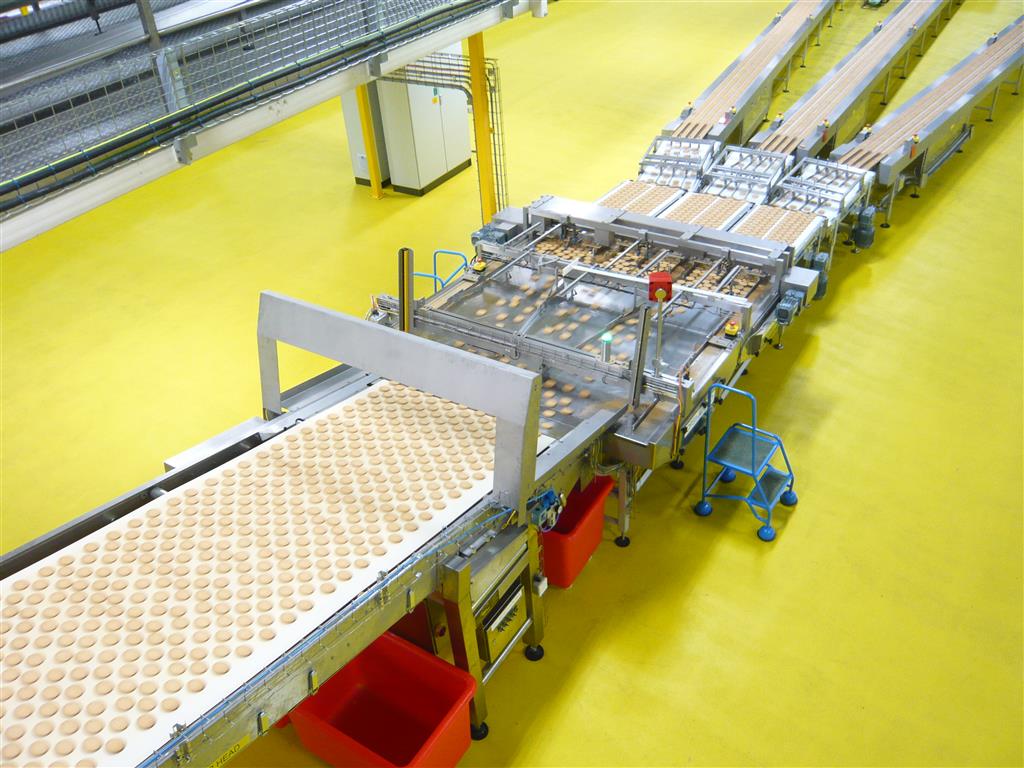
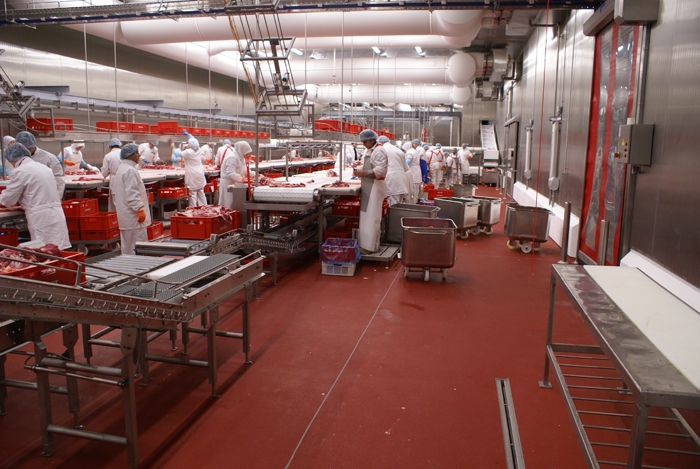
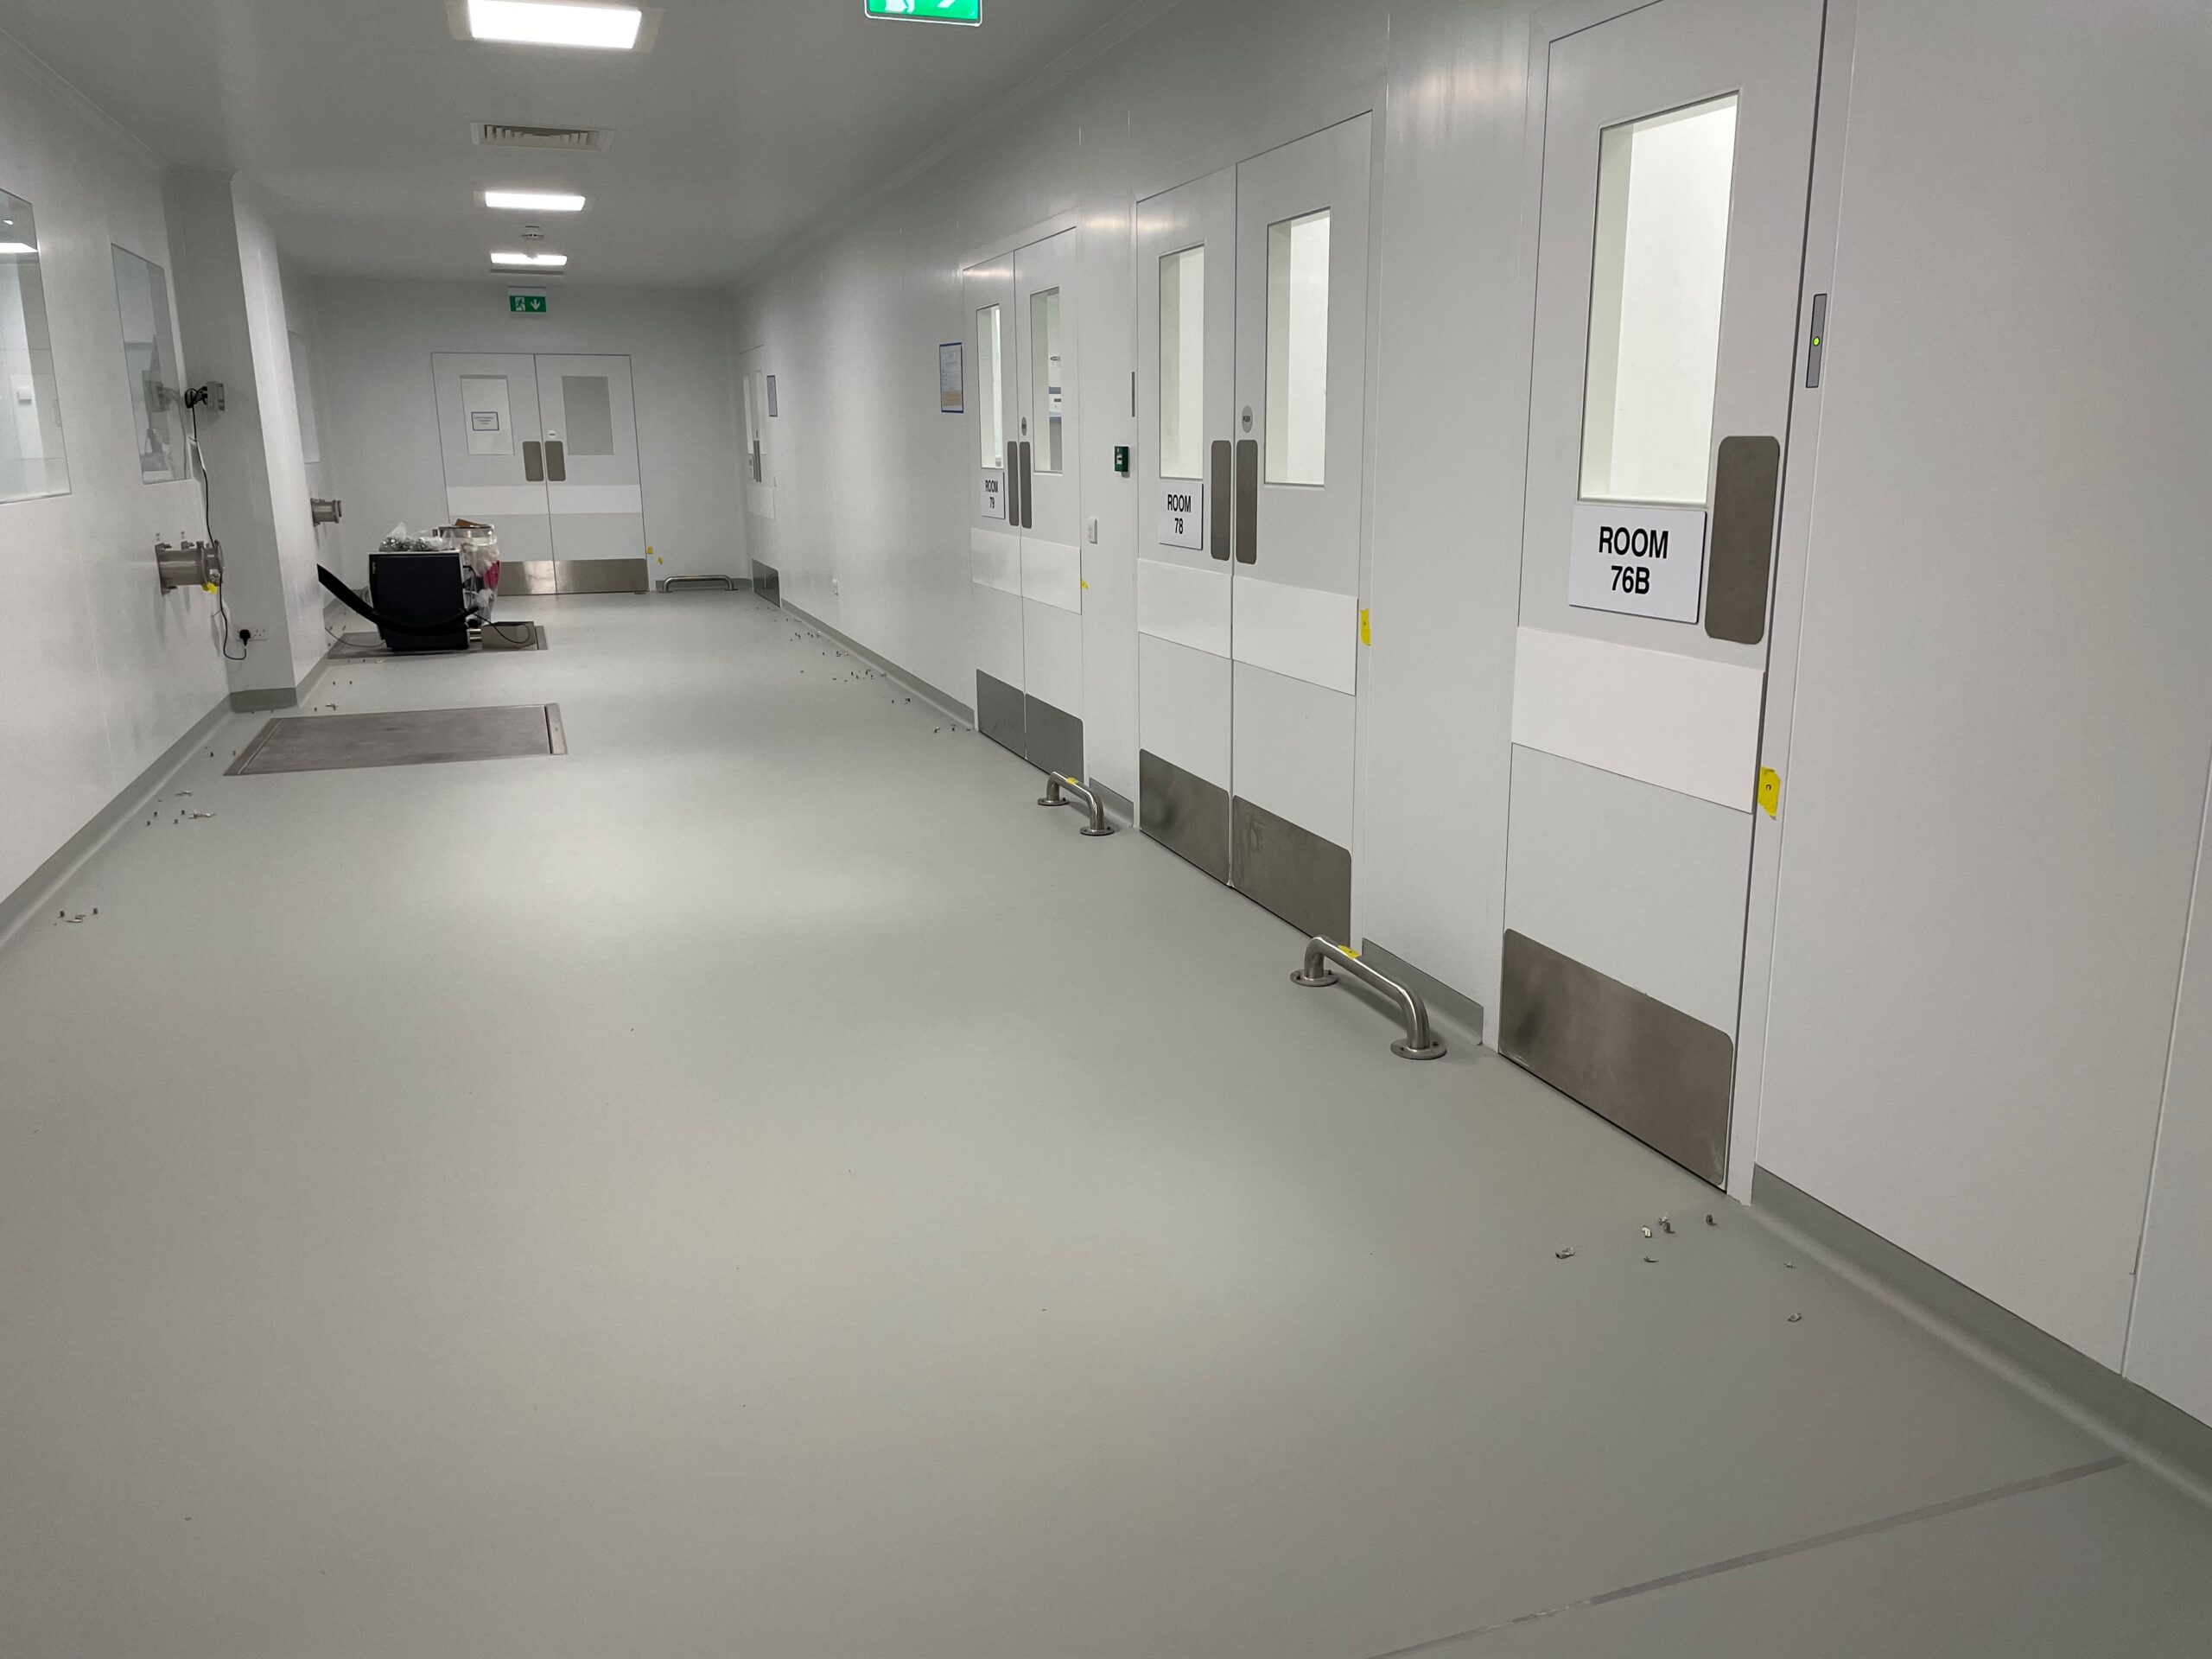
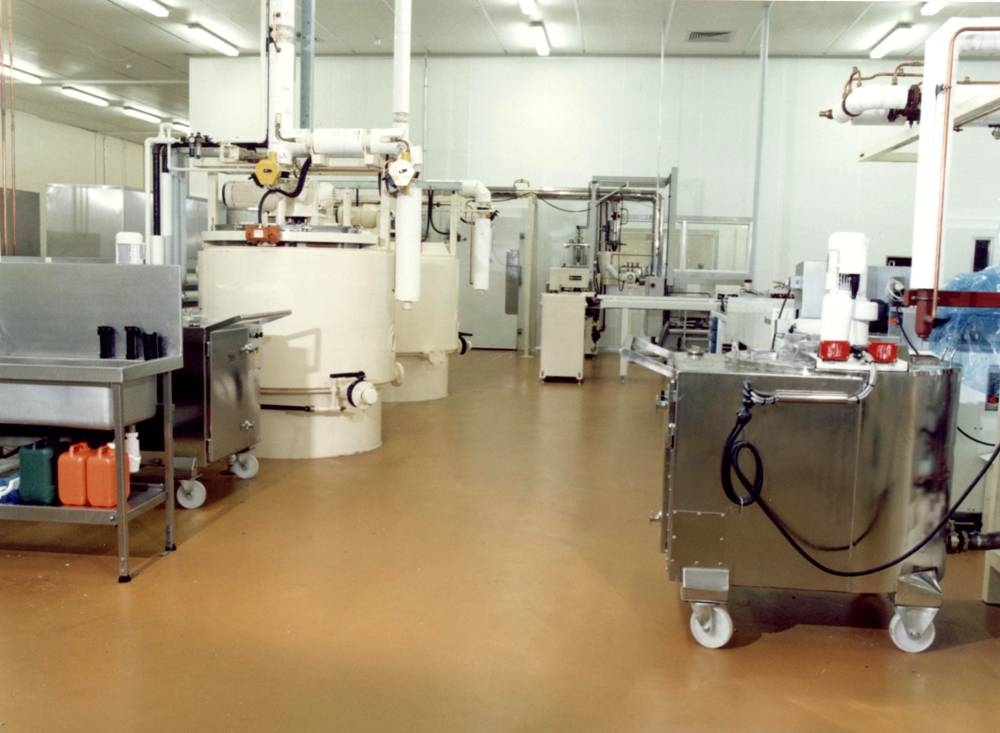
We are market leaders in the specification and application of Polyurethane and Epoxy resin coating and screed systems.
Ancorite is a market leader in the specification and application of Polyurethane and Epoxy resin coating and screed systems offering high performance solutions for a wide variety of commercial and industrial environments. With a focus on durability, safety, chemical resistance, hygiene requirements, traffic and cleaning operations and the expected life of the floor our resin systems are designed to meet the specific requirements where robust flooring is critical.
We provide an extensive range of resin flooring options to suit diverse operational needs:
Available in a variety of finishes, including acrylic concrete hardeners and high-build epoxy coatings. Options include anti-slip quartz aggregates and a range of colours to enhance both safety and aesthetics.
Heavy-duty epoxy and polyurethane systems from 2mm to 9mm, designed for high-impact and heavily stressed environments, with optional anti-static properties.
Decorative quartz, flake epoxy, and fast-curing MMA products for environments that demand both functionality and a premium finish.
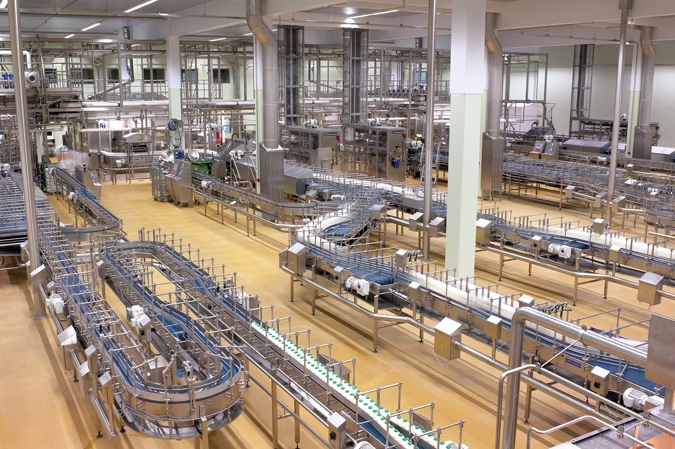
Ancorite’s resin flooring systems are tailored to the unique demands of industries including pharmaceutical, power generation, petrochemical, nuclear, food and beverage, and more. Our floors are engineered to withstand the rigours of heavy traffic, harsh chemicals, and frequent cleaning operations, ensuring long-lasting performance.
Our turnkey resin flooring services include:
– Consultation and system specification to meet operational requirements.
– Installation of resin coatings, screeds, and coving with matching trims in stainless steel or aluminium.
– Anti-slip and decorative finishes to enhance safety and aesthetics.
– Stainless steel drainage channel and kerbing installation.
Resin flooring is a seamless system created by applying liquid resin, such as epoxy or polyurethane, onto a prepared substrate where it cures to form a hard, durable surface.
It provides a non-porous, high-performance finish designed to withstand heavy traffic, chemical exposure, and ongoing industrial wear.
Common resin flooring systems include epoxy, polyurethane (PU), and fast-curing systems such as MMA.
Each system is selected based on specific performance requirements, including chemical resistance, temperature tolerance, curing time, and operational demands.
Resin flooring is widely used in factories, warehouses, food processing facilities, pharmaceutical environments, and cleanrooms.
It is particularly suited to areas requiring a hygienic, durable, and chemically resistant surface.
When correctly specified and installed, resin flooring can provide long-term performance, even in demanding industrial environments.
Its lifespan depends on factors such as traffic intensity, chemical exposure, and maintenance practices.
Selection is based on operational requirements such as load, chemical exposure, temperature conditions, and hygiene standards.
A detailed assessment ensures the system is tailored to the specific performance and compliance needs of the site.