Ancorite provides expert flooring systems tailored to meet the specific needs of diverse industries. With a proven track record, we deliver durable, high-performance flooring systems for various sectors.
Ancorite specialises in the specification, supply, and installation of a wide variety of flooring solutions, including:
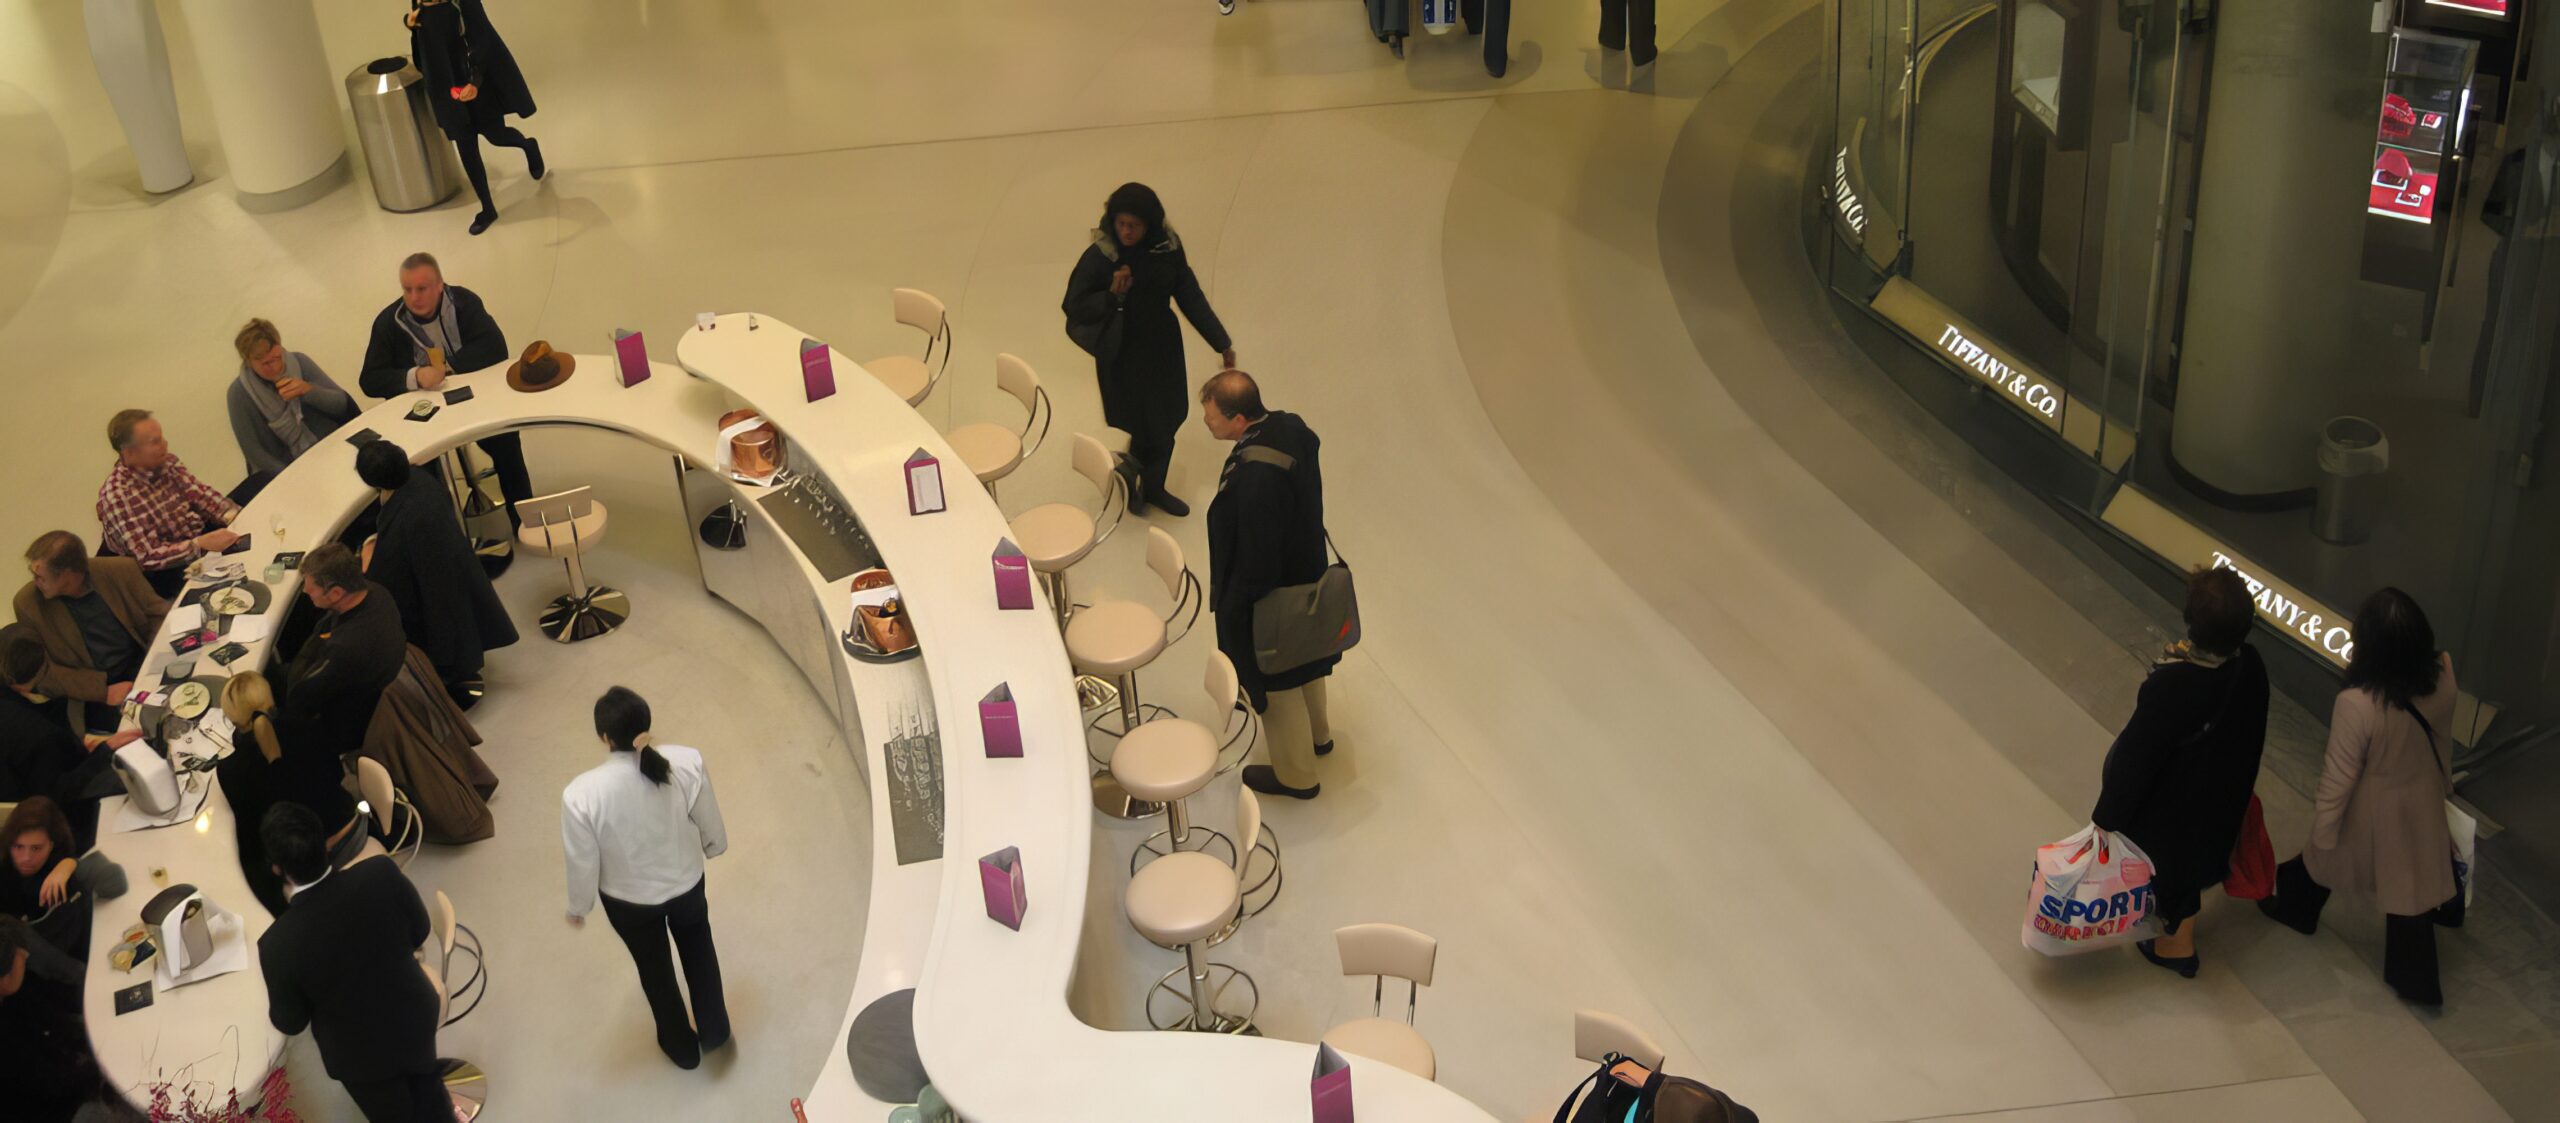
Polished polyurethane and epoxy systems offering durability and aesthetic appeal.
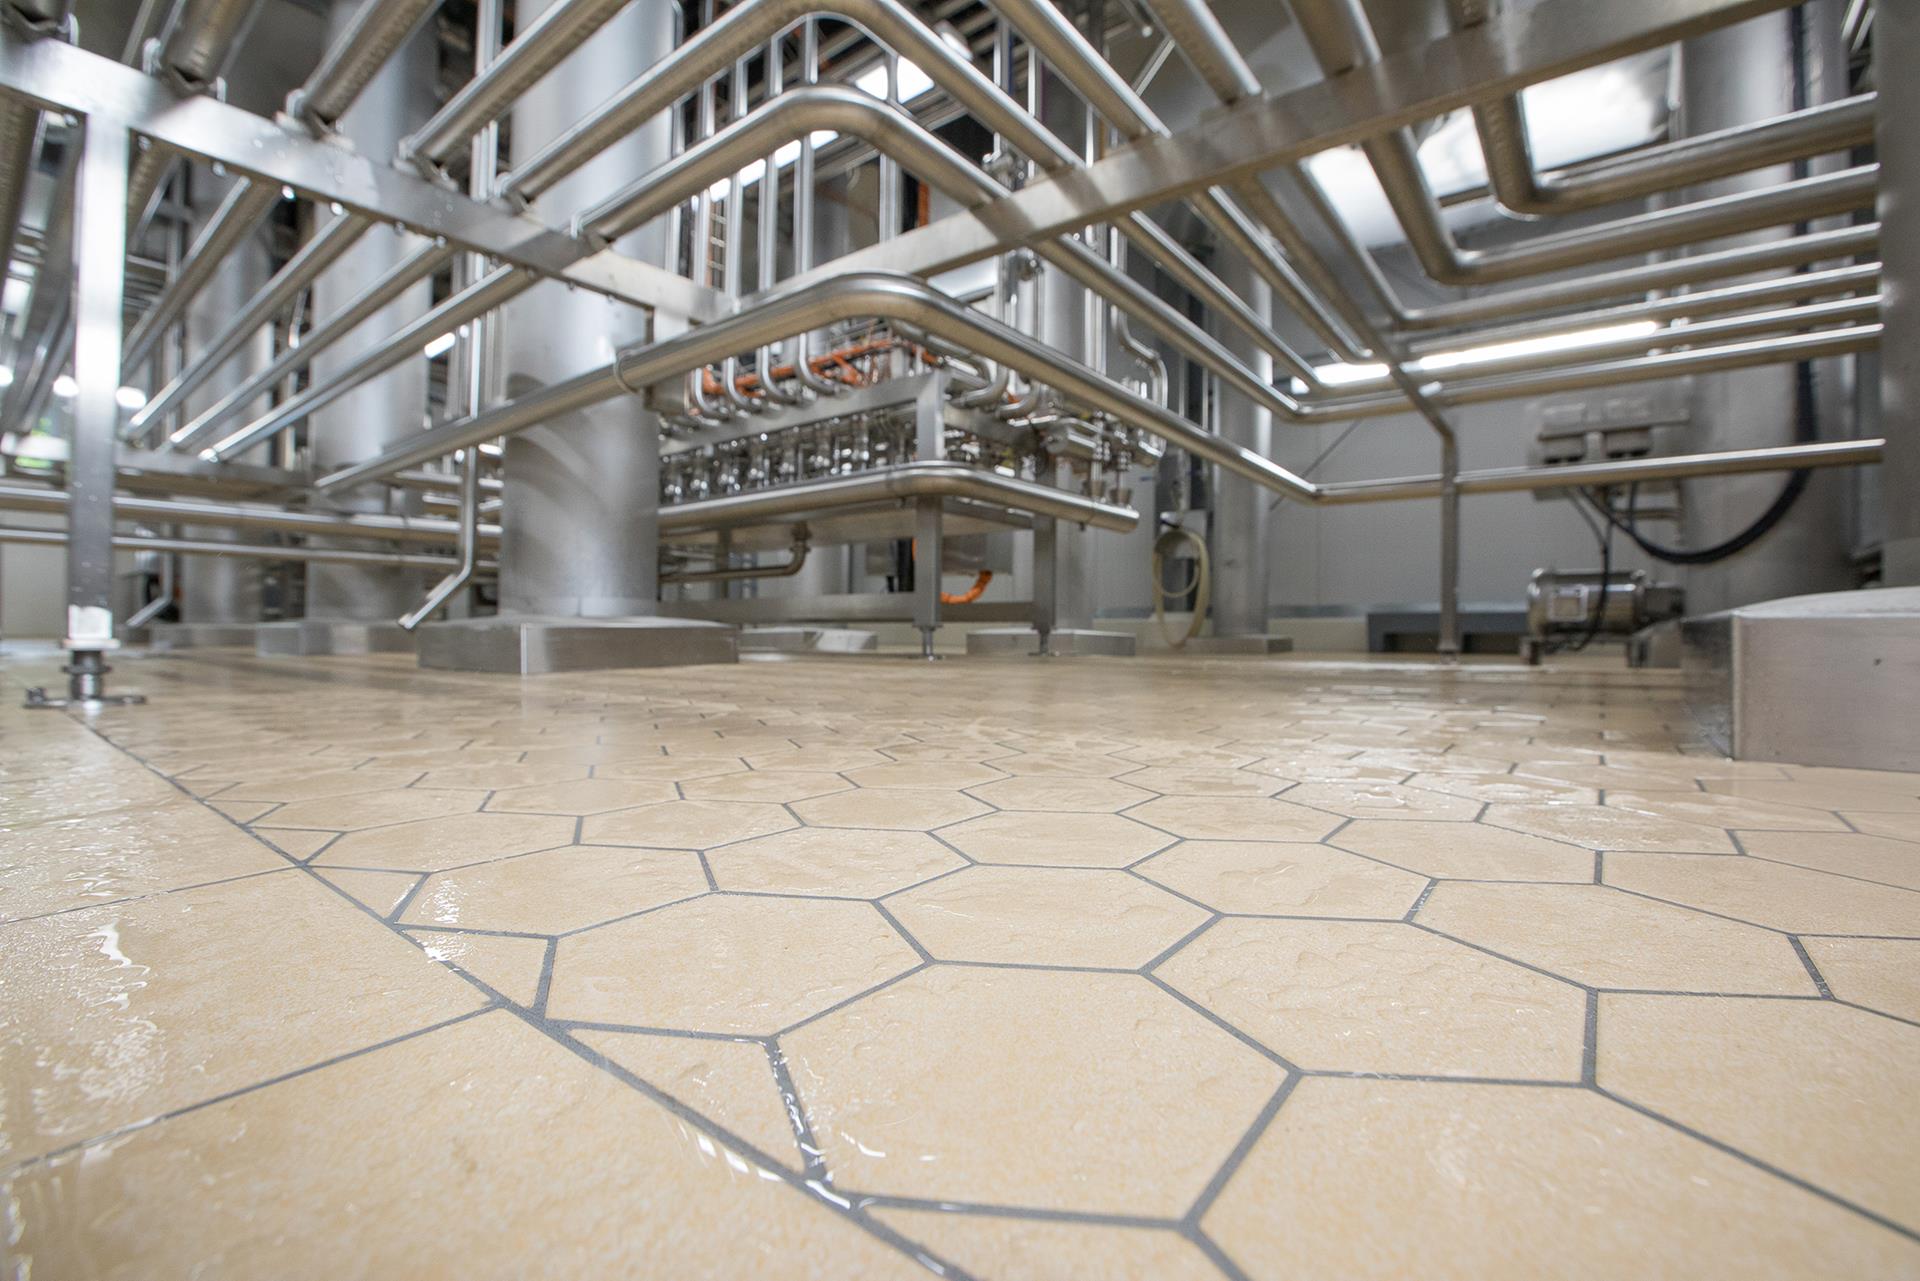
LEARN MOREIncluding vibration, traditional, and chemical-resistant tiling solutions.
LEARN MOREModified screeds, stainless steel channels, and accessories to complete your flooring system.
LEARN MOREOur experienced team works closely with clients to assess their specific requirements and recommend the most suitable flooring system from our extensive range of products. Whether the priority is chemical resistance, hygiene, durability, or aesthetics, Ancorite delivers flooring solutions that meet and exceed expectations. With technical expertise, high-quality materials, and a commitment to excellence, Ancorite is the trusted choice for flooring solutions across a wide array of Industries.
We offer a unique broad range of services in our chosen sectors. We provide a Holistic Offer with the ability to combine the service offerings across our different product range. We are able to react quickly & efficiently to service our customers’ needs. We provide a best-in-class quality service offering. We provide a Professional / Collaborative / Flexible approach.
Specialist industrial flooring is widely used across sectors such as manufacturing, food and beverage, pharmaceutical, chemical processing, and warehousing.
These environments require flooring systems that can withstand heavy traffic, chemical exposure, temperature fluctuations, and strict hygiene or compliance standards.
Epoxy and polyurethane (PU) resin flooring systems are commonly specified for areas exposed to chemicals or heavy traffic due to their strength, durability, and resistance to aggressive conditions.
These systems can be enhanced with anti-slip finishes, protective coatings, or additional layers to meet safety, hygiene, and operational requirements.
Yes – Ancorite delivers industrial flooring installation services across the UK and Ireland, operating from key locations including Cheshire, Teesside, Beverley, and Mayo to support projects efficiently across multiple regions.
A wide range of industrial flooring systems can be installed, including epoxy, polyurethane (PU), and specialist resin flooring solutions. These systems are designed to deliver high durability, chemical resistance, and long-term performance in demanding industrial environments.
Additional options such as anti-slip, anti-static (ESD), and hygienic flooring can be specified for sectors including manufacturing, food processing, and cleanrooms. Each system is selected and installed to meet the operational requirements of the facility.
Resin flooring is a seamless, high-performance system (typically epoxy or polyurethane) designed for durability, chemical resistance, and heavy industrial use. It is often preferred for its practicality, speed of installation, and cost efficiency.
Terrazzo flooring, by contrast, combines aggregates such as marble or stone with a binder to create a decorative yet durable finish. While it offers excellent longevity, it is typically specified where visual appearance is as important as performance.